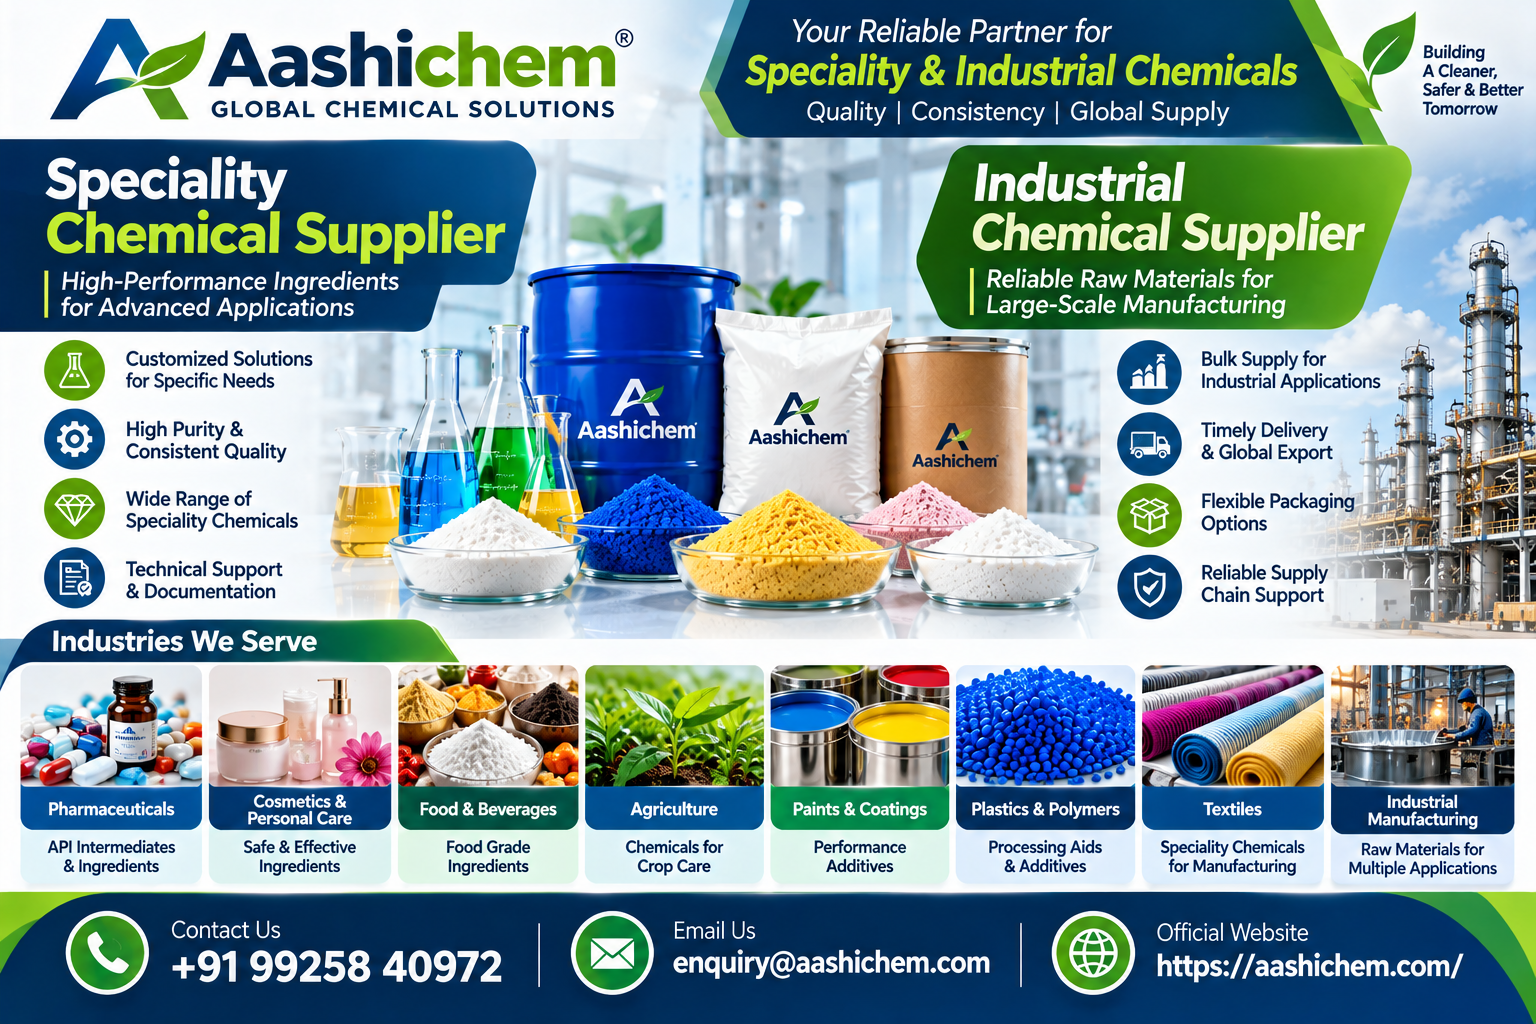
As manufacturers across pharmaceuticals, food processing, personal care, agriculture, coatings, plastics, textiles, construction chemicals, and industrial production seek more reliable sourcing, the role of a professional Speciality Chemical Supplier and dependable Industrial Chemical Supplier is becoming increasingly important. Buyers today expect more than product availability—they also look for consistent specifications, quality documentation, suitable packaging, reliable logistics, and technical support.
Speciality chemicals and industrial chemicals may serve very different functions, but both are essential to modern manufacturing. From additives that improve product performance to bulk chemicals used in large-scale production, supplier quality can influence efficiency, consistency, compliance, and finished-product performance.
What Is a Speciality Chemical Supplier?
A Speciality Chemical Supplier provides chemicals designed for specific functional or performance requirements rather than only general-purpose use.
Speciality chemicals may be used to improve:
- stability
- color
- viscosity
- texture
- adhesion
- preservation
- processing efficiency
- surface performance
- product durability
These chemicals are widely used in industries such as:
- pharmaceuticals
- cosmetics and personal care
- food and nutrition
- paints and coatings
- adhesives
- plastics and polymers
- agriculture
- textiles
- water treatment
Because speciality chemicals often have precise technical functions, correct grade and specification selection are important.
Why Speciality Chemicals Matter
Unlike high-volume commodity chemicals, speciality chemicals are often selected because of the specific result they create in a formulation or process.
For example, manufacturers may require ingredients that:
Improve Product Stability
Certain additives can help formulations remain consistent during storage and use.
Enhance Processing
Processing aids may improve manufacturing efficiency or material handling.
Modify Performance
Specialty additives may influence flexibility, hardness, appearance, or resistance.
Support Formulation Goals
Cosmetic, food, or pharmaceutical products may require carefully selected ingredients to achieve desired sensory or functional characteristics.
What Is an Industrial Chemical Supplier?
An Industrial Chemical Supplier provides chemicals and raw materials used in large-scale manufacturing and industrial processes.
Typical application areas may include:
- metal processing
- detergents and cleaning
- paints and coatings
- plastics
- rubber
- textiles
- construction
- water treatment
- manufacturing processes
Industrial chemicals may be supplied in bulk quantities, depending on customer requirements.
Common packaging formats can include bags, drums, containers, and IBCs.
Speciality Chemicals vs Industrial Chemicals
Although the categories can overlap, their commercial focus is often different.
A Speciality Chemical Supplier generally emphasizes specific performance characteristics and formulation functionality.
An Industrial Chemical Supplier may focus more heavily on volume, process reliability, cost efficiency, and continuous supply.
For some customers, the same supplier may provide both categories.
This can help companies consolidate procurement and simplify supplier management.
Quality Specifications Should Come First
Chemical purchasing should begin with technical requirements.
Important specifications may include:
- assay
- purity
- pH
- moisture
- appearance
- particle size
- viscosity
- residual impurities
- heavy metals where applicable
Manufacturers should share their intended application when requesting quotations.
A supplier can then help identify the most appropriate grade.
Using the wrong grade may cause process issues even if the chemical name is technically correct.
Technical Documentation Builds Confidence
Professional chemical buyers frequently require supporting documents before approving a supplier.
Typical documents may include:
- Certificate of Analysis
- Safety Data Sheet
- Technical Data Sheet
- product specification
- storage instructions
- shelf-life information
Regulated industries may require additional documentation.
An experienced Speciality Chemical Supplier should understand the importance of providing accurate technical information for customer review.
Batch Consistency Supports Reliable Manufacturing
For repeat production, manufacturers expect chemicals to behave consistently from one batch to another.
Variation can affect:
- reaction performance
- viscosity
- color
- product stability
- process temperature
- finished-product quality
A reliable Industrial Chemical Supplier should maintain clear batch identification and dependable sourcing.
Customers may also request pre-shipment testing or samples before approving large-volume orders.
Packaging Protects Chemical Quality
Chemical packaging is not simply a transportation requirement—it is part of product protection.
Packaging selection may depend on:
- physical form
- moisture sensitivity
- chemical compatibility
- shipment quantity
- storage conditions
Possible formats include:
Bags
Common for powders and granular materials.
Drums
Frequently used for liquids, powders, and specialty products.
IBC Containers
Suitable for larger quantities of certain liquid chemicals.
Customized Packaging
Some customers may require specific pack sizes for production efficiency.
A professional supplier should ensure packaging is suitable for the material being supplied.
Chemical Supply for Pharmaceuticals
Pharmaceutical manufacturers may require carefully controlled raw materials and intermediates.
Important considerations can include:
- purity
- traceability
- documentation
- consistent specifications
- storage conditions
A Speciality Chemical Supplier serving this sector should understand that customer qualification may be more detailed than in general industrial applications.
Chemicals for Cosmetics and Personal Care
Personal-care manufacturers use speciality ingredients in:
- skincare
- haircare
- cleansers
- toiletries
- beauty products
The supplier may need to provide information related to ingredient identity, specification, storage, and compatibility.
Cosmetic formulators often prioritize both technical performance and sensory characteristics.
Chemicals for Paints and Coatings
Paint and coating manufacturers may require chemicals that influence:
- flow
- dispersion
- drying
- adhesion
- color
- surface performance
A dependable Industrial Chemical Supplier can help ensure raw-material availability for continuous production.
Stable supply is especially important for high-volume coating manufacturers.
Agriculture and Industrial Formulations
Chemical ingredients are also widely used in agricultural formulations and industrial processes.
Potential applications include:
- crop-care formulations
- fertilizers
- cleaning chemicals
- processing aids
- industrial treatments
Each application may require different purity levels, packaging formats, and handling instructions.
Supply Reliability Is Becoming More Important
Manufacturing companies increasingly evaluate suppliers based on supply-chain resilience.
Key factors include:
- product availability
- production capacity
- lead time
- inventory planning
- documentation
- packaging options
- logistics capability
- export experience
- communication
- consistency
Unexpected delays in raw materials can interrupt entire production lines.
For this reason, supply reliability is often considered as important as pricing.
Global Export and Logistics Support
Many chemical manufacturers source internationally.
A supplier serving global customers should understand:
- export packaging
- shipping documentation
- product labeling
- container planning
- delivery timelines
An experienced Industrial Chemical Supplier can coordinate these details more efficiently, reducing the administrative burden on buyers.
Frequently Asked Questions
What is a Speciality Chemical Supplier?
A Speciality Chemical Supplier provides chemical ingredients designed for specific performance, formulation, or processing requirements.
What industries use speciality chemicals?
Pharmaceuticals, cosmetics, food, agriculture, coatings, plastics, textiles, adhesives, and many other industries use speciality chemicals.
What is an Industrial Chemical Supplier?
An Industrial Chemical Supplier provides chemicals and raw materials used in manufacturing and large-scale industrial processes.
What documents should chemical suppliers provide?
Common documents include a Certificate of Analysis, Safety Data Sheet, Technical Data Sheet, and product specification.
Why is purity important?
Purity can directly affect processing, formulation performance, and finished-product consistency.
Can speciality chemicals be supplied in bulk?
Yes. Depending on the product and customer requirements, speciality chemicals can be supplied in commercial or bulk quantities.
What packaging options are commonly available?
Common formats include bags, drums, plastic containers, and IBCs.
Can buyers request samples?
Many suppliers can provide samples depending on the product and commercial conditions.
Why is batch consistency important?
Consistent batches help manufacturers maintain stable processes and predictable finished-product quality.
What information should buyers provide for a quotation?
Useful information includes chemical name, grade, specification, quantity, packaging requirement, destination, and intended application.
Media Contact
Speciality & Industrial Chemical Enquiries
Contact: +91 99258 40972
Email: enquiry@aashichem.com
Official Website: https://aashichem.com/