Metal fabrication is becoming increasingly responsive to custom orders, shorter production runs, tighter delivery schedules, and diverse component designs. This shift is encouraging workshops to reconsider how forming operations are organized, particularly when large machines are not the most efficient option for every job.
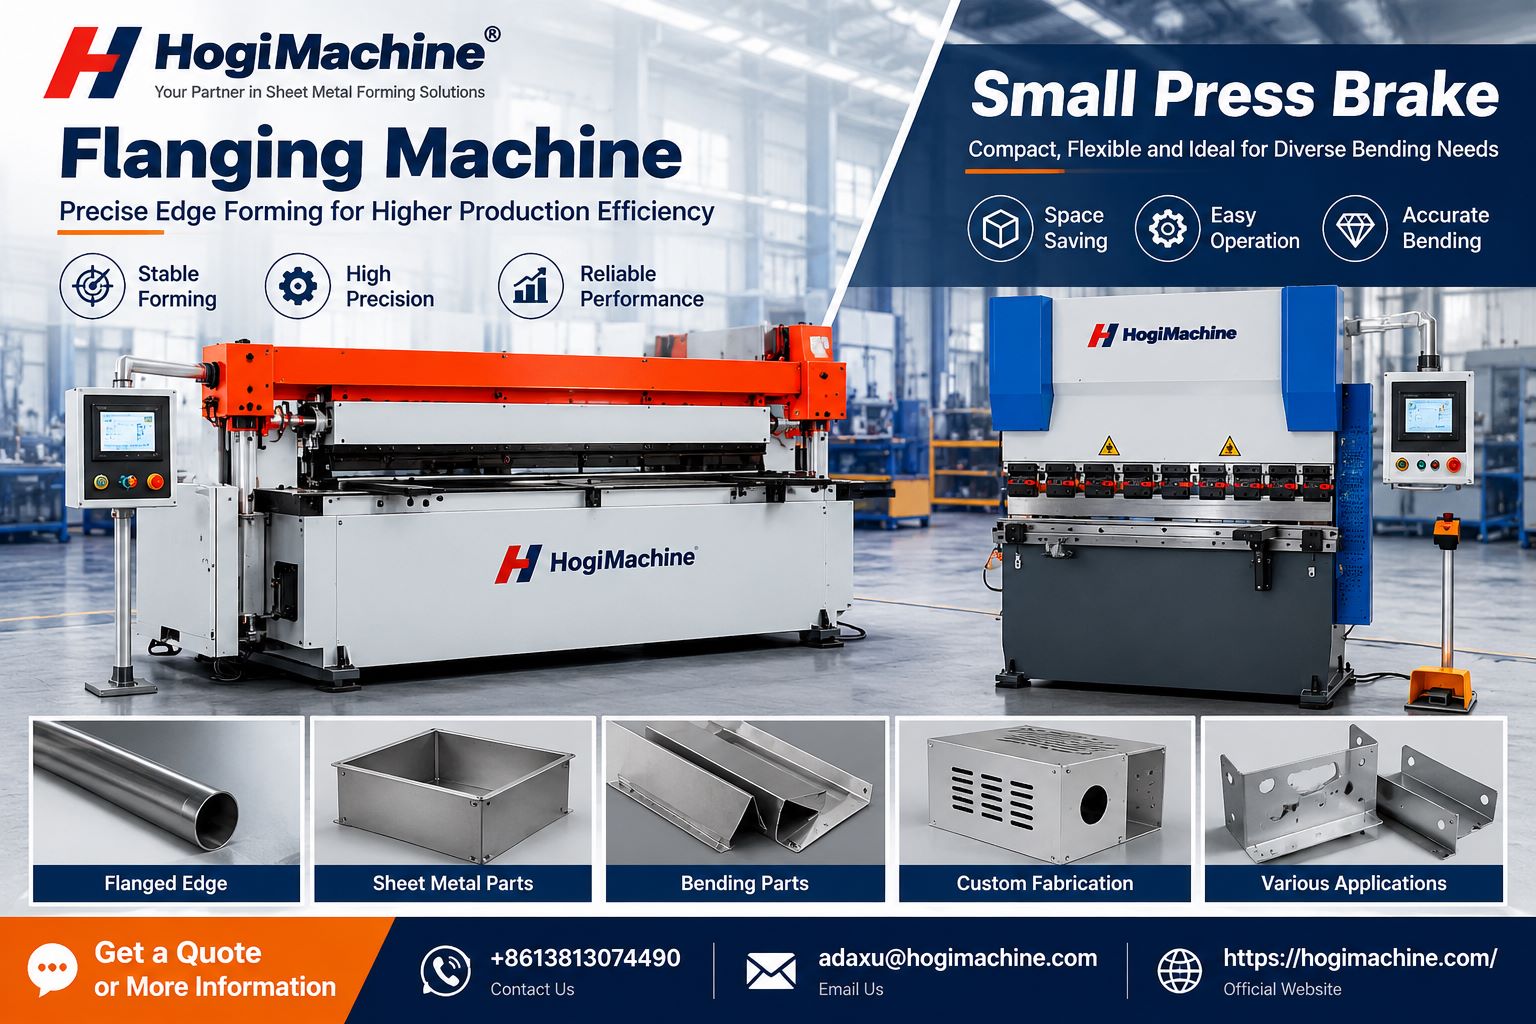
Two technologies are becoming particularly relevant within this changing environment: the Flanging machine, which supports controlled edge-forming operations, and the small press brake, which provides compact bending capability for suitable sheet-metal components. Used within a well-planned workflow, these machines can help manufacturers allocate jobs more efficiently while maintaining production flexibility.
Flanging Is Becoming a More Specialized Production Step
Flanging creates a formed edge or lip on a metal workpiece. Depending on the product, that flange may assist with joining, assembly, reinforcement, positioning, or subsequent manufacturing.
Although seemingly straightforward, achieving consistent flange geometry requires control over material behavior and the forming process.
A dedicated Flanging machine allows manufacturers to approach this operation as a repeatable production stage rather than an improvised task.
This can be especially useful for factories that manufacture similar flanged components regularly and want to establish standardized procedures.
Job Routing Can Improve Fabrication Efficiency
One emerging strategy in metalworking is smarter job routing.
Instead of sending every component to the largest available forming machine, production managers can assign work according to actual requirements.
Large equipment can remain available for components that genuinely need its capacity, while smaller work can be directed to more appropriately sized machines.
A small press brake can play an important role in this strategy by handling suitable compact parts without unnecessarily occupying larger bending equipment.
The result can be a more balanced production environment.
Small Press Brake Technology Supports Custom Manufacturing
High-mix manufacturing creates different challenges from continuous mass production.
A fabrication workshop may need to manufacture brackets in the morning, enclosure components later in the day, and prototype parts for another customer afterward.
For suitable applications, a small press brake can provide the versatility required for this type of workload.
Its value is particularly noticeable when manufacturers need frequent setup changes and relatively short bend lengths.
Machine selection should nevertheless be based on the required forming force, workpiece dimensions, material type, thickness, tooling, and intended production quantity.
Forming Capacity Must Match the Actual Job
Selecting sheet-metal equipment based only on general descriptions can lead to poor purchasing decisions.
Before choosing a machine, manufacturers should examine the parts they intend to produce.
Material strength, sheet thickness, bend or flange length, geometry, tooling, and production volume can all influence machine requirements.
For a Flanging machine, buyers should also consider the type of flange being produced and how the workpiece will be handled during production.
For press brake operations, available forming capacity should always be respected.
Prototype Work Benefits From Flexible Forming Capacity
Product development frequently requires manufacturers to produce small quantities before committing to larger production.
Prototypes allow designers to evaluate component dimensions, assembly, appearance, and manufacturability.
Compact bending equipment can be useful during this stage because development teams may need several design revisions.
A small press brake can provide dedicated capacity for suitable prototype components while allowing larger production equipment to continue working on established orders.
This separation can help workshops avoid interrupting major production schedules for every small development job.
Flanging Quality Can Affect Downstream Assembly
The quality of a formed flange can influence more than the appearance of an individual component.
If the flange is used as an assembly interface, inconsistent geometry may create problems later in production.
Components may become difficult to position, align, join, or fit with mating parts.
Repeatable Flanging machine operation therefore supports downstream manufacturing as well as the forming stage itself.
Production teams should define the important flange characteristics and establish suitable checks according to the component’s functional requirements.
Tooling Management Is Critical for Repeat Jobs
Tooling should be treated as part of the manufacturing process rather than as an accessory.
Correct tooling selection helps create the required component geometry and supports repeatability.
Workshops handling many product variants can benefit from organized tooling management.
Frequently used tooling should be stored properly, identified clearly, and inspected for wear or damage. Setup information for repeat components can also be documented.
For a small press brake, organized tooling and job records can shorten the time needed to prepare recurring orders.
Similar practices can support consistent flanging operations.
Operator Ergonomics Deserve Attention
Manufacturing efficiency is closely connected to how operators interact with equipment.
If employees repeatedly lift, rotate, reposition, or support awkward components, productivity and handling quality may be affected.
Workpiece size and weight should therefore be considered when planning the forming station.
For compact parts, appropriately positioned equipment and material staging can help create a smoother workflow.
Controls, tooling access, workpiece handling, and inspection areas should be arranged with practical operation in mind.
Digital Job Records Can Support Repeatability
Many fabrication businesses manufacture the same components repeatedly, sometimes with long intervals between orders.
Depending entirely on operator memory can make future setups more difficult.
Digital or controlled job records can preserve useful information about tooling, bend sequences, machine settings, material, and inspection requirements where appropriate.
When the next order arrives, production teams have a more structured starting point.
This can be particularly valuable for high-mix operations using a small press brake, where many different jobs may pass through the same workstation.
Preventive Maintenance Helps Protect Availability
Flexible production requires machines to be ready when jobs arrive.
Unexpected breakdowns can disrupt schedules, particularly in workshops operating with limited backup capacity.
Preventive maintenance helps reduce this risk.
Inspection schedules should reflect machine design, operating hours, workload, and manufacturer guidance. Tooling condition should also be checked because worn or damaged tools can influence component quality.
Maintaining a Flanging machine and press brake systematically can support both equipment availability and production consistency.
Frequently Asked Questions
What is a Flanging machine?
A Flanging machine is forming equipment used to create a flange, lip, or formed edge on a metal component according to the intended manufacturing or assembly requirement.
What is a small press brake used for?
A small press brake is commonly used for suitable compact sheet-metal bending jobs, including brackets, panels, prototypes, enclosures, repair components, and short production runs.
What is the main benefit of dedicated flanging equipment?
Dedicated equipment can help manufacturers establish a controlled and repeatable process for recurring edge-forming operations.
Why choose a compact press brake?
Compact equipment can provide flexible bending capacity while using less production space than substantially larger machinery.
Can a small press brake handle production work?
Yes, provided the material, workpiece dimensions, forming requirements, and workload remain within the machine’s specified capabilities.
What factors affect metal bending?
Material type and strength, thickness, bend length, geometry, tooling, and forming conditions can all influence results.
Why are job records useful?
Job records can preserve tooling and setup information, helping operators prepare repeat orders more efficiently.
How does tooling influence forming accuracy?
Appropriate tooling helps establish the required geometry and supports consistent forming when used within suitable machine and material limits.
Why is preventive maintenance important?
Regular inspection and maintenance can help identify developing issues before they result in unexpected downtime or production problems.
What should buyers consider before purchasing forming equipment?
Buyers should evaluate their actual component range, materials, thicknesses, working dimensions, forming capacity, tooling requirements, available factory space, operator workflow, and after-sales support.
Media Contact
Sheet Metal Forming Equipment Enquiries
Contact: +86 138 1307 4490
Email: adaxu@hogimachine.com
Official Website: hogimachine.com